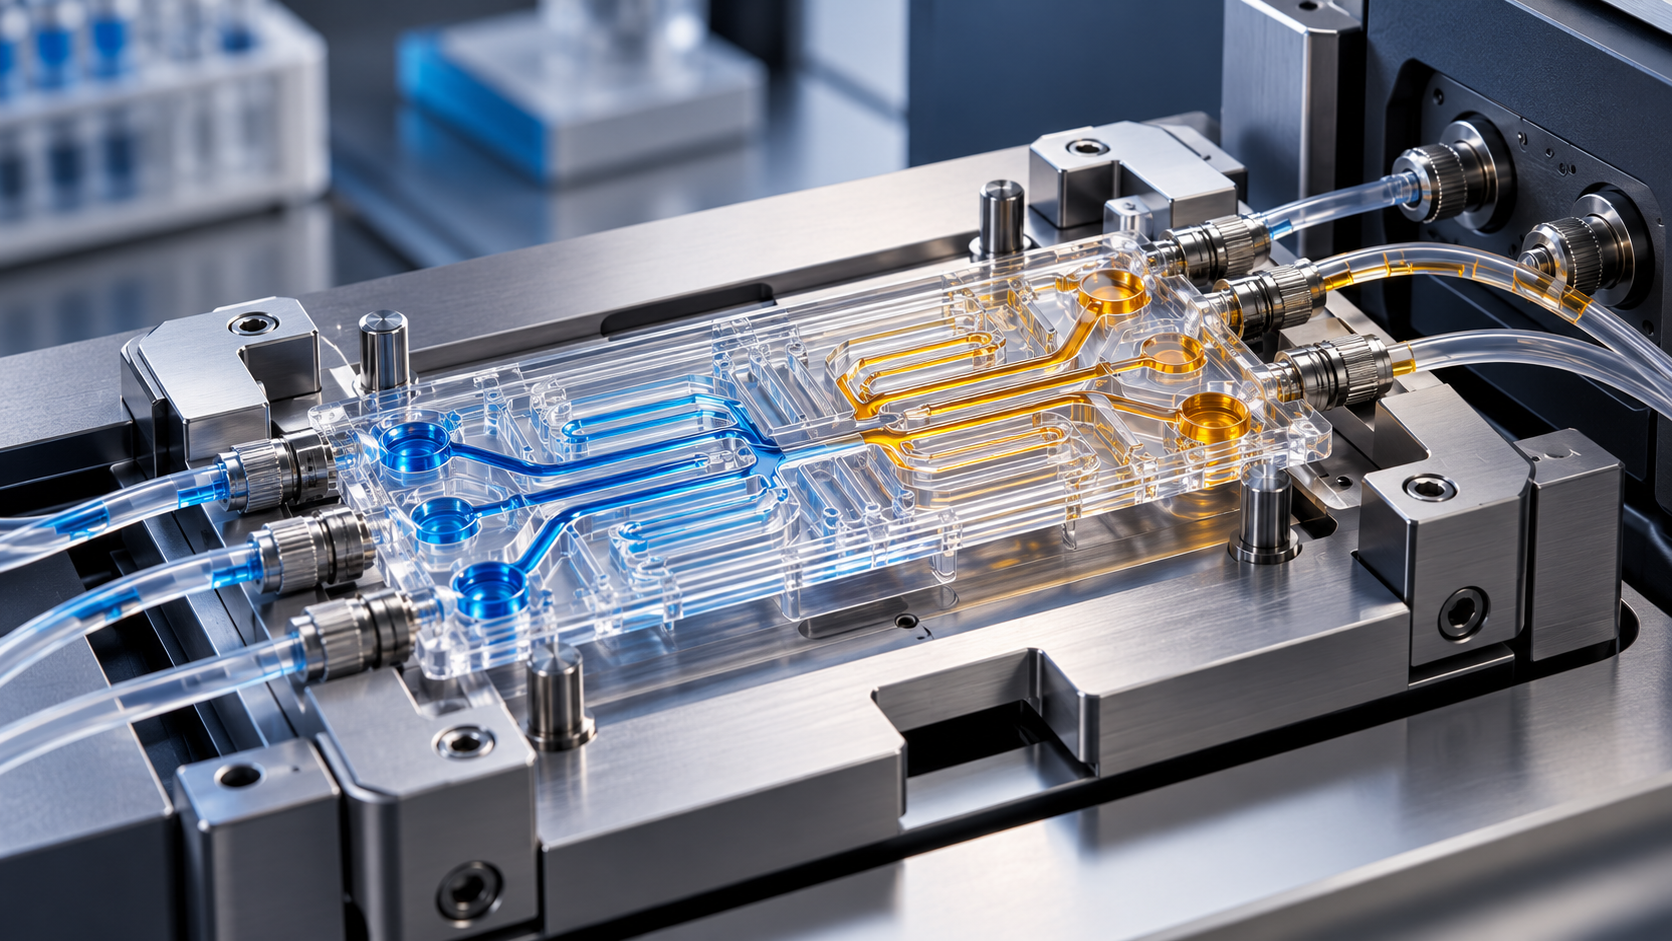
Microfluidic Interoperability Moves Toward Manufacturing
Microfluidic interoperability is becoming a practical manufacturing question. A draft revision of the interface standard and renewed attention to commercialization at MicroTAS signal movement toward reusable components and clearer operating specifications. Common footprints and port descriptions could reduce integration effort, but they cannot establish leakage performance, fluid compatibility or assay validity. The strategic opportunity lies in qualifying the boundary between the disposable cartridge and the reusable instrument.
MEMSWork Intelligence Dashboard
| Field | Assessment |
|---|---|
| Market status | Commercial devices coexist with custom research systems; cross-vendor interchangeability remains application-dependent. |
| Primary constraint | Separating mechanical compatibility from validated fluidic and analytical performance. |
| Demand driver | Repeatable lab automation, replaceable cartridges and transferable organ-on-chip workflows. |
| Time horizon | Standards development is active; supplier adoption and qualification timing remain uncertain. |
| Technologies to watch | Cartridge fixtures, low-dead-volume connections, leakage tests, traceable flow measurement and machine-readable specifications. |
| Strategic signal | Interface documentation and verification could become reusable supplier assets. |
| Next trigger | Final revision text and independent demonstrations of interchangeable components under a declared operating window. |
What changed in microfluidic interoperability
On September 28, 2026, ISO registered ISO/DIS 22916, a draft revision addressing microfluidic dimensions, connections and device classification. The public record lists it as under development, intended to replace ISO 22916:2022. Registration is a standards-development milestone, not publication of a replacement standard or evidence of market adoption.
The timing is useful. The MicroTAS 2026 program for October 18–22 in Granada includes workshops on manufacturing, standardization and commercialization. Its manufacturing session brings together NIST, universities and suppliers including Fluigent and microfluidic ChipShop. The program demonstrates attention to translation; it does not establish what attendees achieved or constitute a new industry agreement.
The decision question for an instrument company is straightforward: can a cartridge from a different supplier be installed, controlled and replaced without repeating the entire integration project? A connector that physically fits answers only part of that question. The instrument must also know which fluid, pressure, temperature, flow conditions and cleaning procedures the assembly can tolerate.
A clearer interface can preserve design freedom
The MFMET II revision whitepaper, published January 30, 2026, proposes finer footprint choices, space for clamping hardware, structured descriptions of port positions and device sub-regions, and a framework for declaring an operating window. It also proposes clarifying the boundary between microfluidic interconnections and conventional fluid-handling connections. These are the authors’ proposals; the public ISO status page does not prove that every proposal will appear in the final text.
That approach matters commercially because standardizing an external boundary need not standardize the internal channel architecture. A developer can retain proprietary mixing, separation, sensing or cell-culture structures while making the cartridge easier to hold and connect. In MEMSWork’s assessment, this is the useful compromise: preserve differentiation inside the device while making integration requirements explicit at its perimeter.
It also changes the design handoff. A drawing of the channel network is insufficient for a manufacturing partner. The handoff should identify reference surfaces, port coordinates, sealing regions, fixture loads and acceptance tests. A machine-readable description could support automated checking, but only if suppliers agree on semantics, tolerances and version control. Textual portability alone cannot guarantee physical interchangeability.
Compatibility and qualification require different evidence
| Evidence layer | What it can establish | What remains to prove |
|---|---|---|
| Dimensions and port locations | A defined interface for fixture and connection design | Assembly tolerances and cross-supplier fit |
| Declared operating window | Conditions a supplier says the device supports | Test methods, uncertainty and performance across batches |
| External leakage testing | Containment under the tested conditions | Internal bypass, contamination and application-specific lifetime |
| Flow metrology | A traceable reference for delivered flow | Behavior with the actual fluid and assembled instrument |
| Application validation | Useful performance in the intended workflow | Transfer across users, sites and replacement lots |
The Microfluidics Association’s leakage-testing guideline, hosted by NIST, specifically addresses unintended outward release to the environment. Its stated scope does not resolve internal leakage within the system. This distinction prevents a dangerous procurement shortcut: a device can contain fluid externally while allowing an internal bypass that changes residence time, concentration or sample routing.
Flow needs its own evidence. NIST reports standards measuring 1 µL per minute with uncertainty below 1%. That is a metrology capability, not an accuracy specification for every microfluidic instrument. Qualification must connect the reference measurement to the assembled system, its fluid and its operating conditions. A calibration with a reference liquid cannot, by itself, establish behavior with a complex biological sample.
Manufacturing economics depend on the whole interface
The NIST-hosted standardization perspective identifies gaps spanning flow control, interconnections, integration, manufacturing, assembly, packaging, reliability and safety. The implication for procurement is that the channel fabrication quote captures only part of product cost. Fixtures, seals, inspection, assembly labor, calibration, failed runs and replacement logistics can determine whether a nominally inexpensive cartridge is economical.
A useful supplier comparison should therefore track cost per accepted, usable cartridge and per successful workflow. Teams should record assembly time, first-pass acceptance, leakage-related rejects, calibration effort and replacement consistency. Those are proposed diligence metrics, not a claimed industry benchmark. Public evidence does not support a universal percentage saving from adopting the interface standard.
This extends MEMSWork’s analysis of supplier qualification in advanced packaging: compatible components become valuable when their process interactions are understood. In microfluidics, the critical boundary includes fluids and surfaces as well as geometry. The standard can simplify an engineering conversation; qualification must supply the missing performance evidence.
Where suppliers and partnerships can create value
The landscape includes cartridge fabricators, instrument OEMs, connector and seal suppliers, flow-control vendors, metrology laboratories and application developers. The MicroTAS program’s mix of researchers and commercial participants illustrates that breadth. It should not be read as proof that any named vendor has qualified products against the draft revision.
For a startup, the defensible asset may be a verified interface package: controlled drawings, inspection records, material declarations, test methods and evidence that replacement cartridges preserve workflow performance. For an instrument OEM, the strategic benefit could be a qualified alternative supplier without changing the application. Both propositions require actual substitution trials before they support a sourcing or investment decision.
Software interoperability is complementary. MEMSWork’s analysis of hardware orchestration for laboratory automation concerns discovery and control above the instrument. A shared command interface cannot correct a leaking seal or an incompatible cartridge. Conversely, a repeatable physical interface still needs explicit control limits and error reporting to work reliably in an automated laboratory.
What to Watch Over the Next 12 Months
- Standards status: changes in the ISO draft’s scope, enquiry status and eventual publication; distinguish proposals from adopted text.
- Supplier documentation: drawings and operating-window declarations tied to named product versions and test methods.
- Substitution trials: different suppliers’ cartridges tested in the same fixture and instrument without undisclosed adapters or manual tuning.
- Manufacturing statistics: dimensional acceptance, leakage rejects and workflow performance across production lots.
- Metrology transfer: traceable flow and pressure checks under representative fluids and assembled-system conditions.
- Customer adoption: repeat procurement and qualified alternative sources, rather than conference participation or a compatibility claim alone.
What Would Change the Thesis?
The thesis would strengthen if published interface declarations allow independent suppliers to replace cartridges while preserving the customer’s acceptance criteria. Evidence of less integration work, lower rejection cost and stable performance across lots would make the commercial case materially stronger.
It would weaken if nominally compatible components still require custom fixtures, extensive recalibration or supplier-specific handling. It would need revision if application requirements force such different sealing, materials or operating envelopes that a common boundary adds more adaptation work than it removes. A final standard without supplier uptake would be a documentation milestone, not an ecosystem transition.
Takeaway
Microfluidic standardization is reaching a useful decision point: interface definitions can become procurement specifications. The commercial prize is repeatable integration and replacement. The next evidence must connect geometry, containment, flow measurement and application performance in the same assembled system. Until that evidence exists, interoperability should remain a testable engineering claim.
Sources and Methodology
This analysis uses public standards status records, a revision proposal, a current conference program and foundational metrology and testing sources. The full paid ISO draft was not reviewed. Proposed changes are attributed to MFMET rather than assumed to be adopted ISO requirements. No market-size estimate, claimed cost saving or forecast adoption date is used.
- ISO/DIS 22916 development record
- ISO 22916:2022 published scope
- MFMET II revision whitepaper
- MicroTAS 2026 workshop program
- Reyes-Hernandez et al., standardization and commercialization
- Microfluidics Association, Protocols for leakage testing
- NIST, Flow and Pressure
Published October 21, 2026. Last updated October 21, 2026. Update history: initial publication.